Direct Engineering Conclusion: An exhaustive engineering guide to Cosine's zero-defect quality architecture conforming to ISO 9001:2015 and IATF 16949. Explore our 100% CP wafer probing, tri-temperature (-40°C, +25°C, +125°C) final test screening, statistical Cpk > 1.67 process control, and AEC-Q001 Part Average Testing eliminating outlier failures before shipment.
An exhaustive engineering guide to Cosine's zero-defect quality architecture conforming to ISO 9001:2015 and IATF 16949. Explore our 100% CP wafer probing, tri-temperature (-40°C, +25°C, +125°C) final test screening, statistical Cpk > 1.67 process control, and AEC-Q001 Part Average Testing eliminating outlier failures before shipment.
1. The Philosophy of Total Quality: Beyond Statistical Acceptance
In modern industrial automation, automotive electronics, and mission-critical renewable power systems, semiconductor quality cannot be treated as a downstream sorting operation. When an analog integrated circuit fails in a solar string inverter operating on a remote mountain plateau or in an electric vehicle battery management system traveling at highway speeds, the consequences extend far beyond component replacement costs. A single field failure triggers emergency service truck rolls, vehicle recalls, customer brand damage, and catastrophic warranty liabilities that dwarf the unit cost of the silicon by orders of magnitude.
Cosine Nanoelectronics was founded on an uncompromising principle: The Zero-Defect Standard. Quality is not an afterthought checked at the end of a manufacturing line; it is an architectural discipline embedded into every stage of our operations—from transistor-level layout symmetry and dual-foundry BCD wafer fabrication to 100% tri-temperature automated testing and closed-loop 8D failure analysis. Operating under certified ISO 9001:2015 and automotive IATF 16949 quality management systems, Cosine delivers analog silicon with proven field defect rates below 0.5 DPPM (defective parts per million).
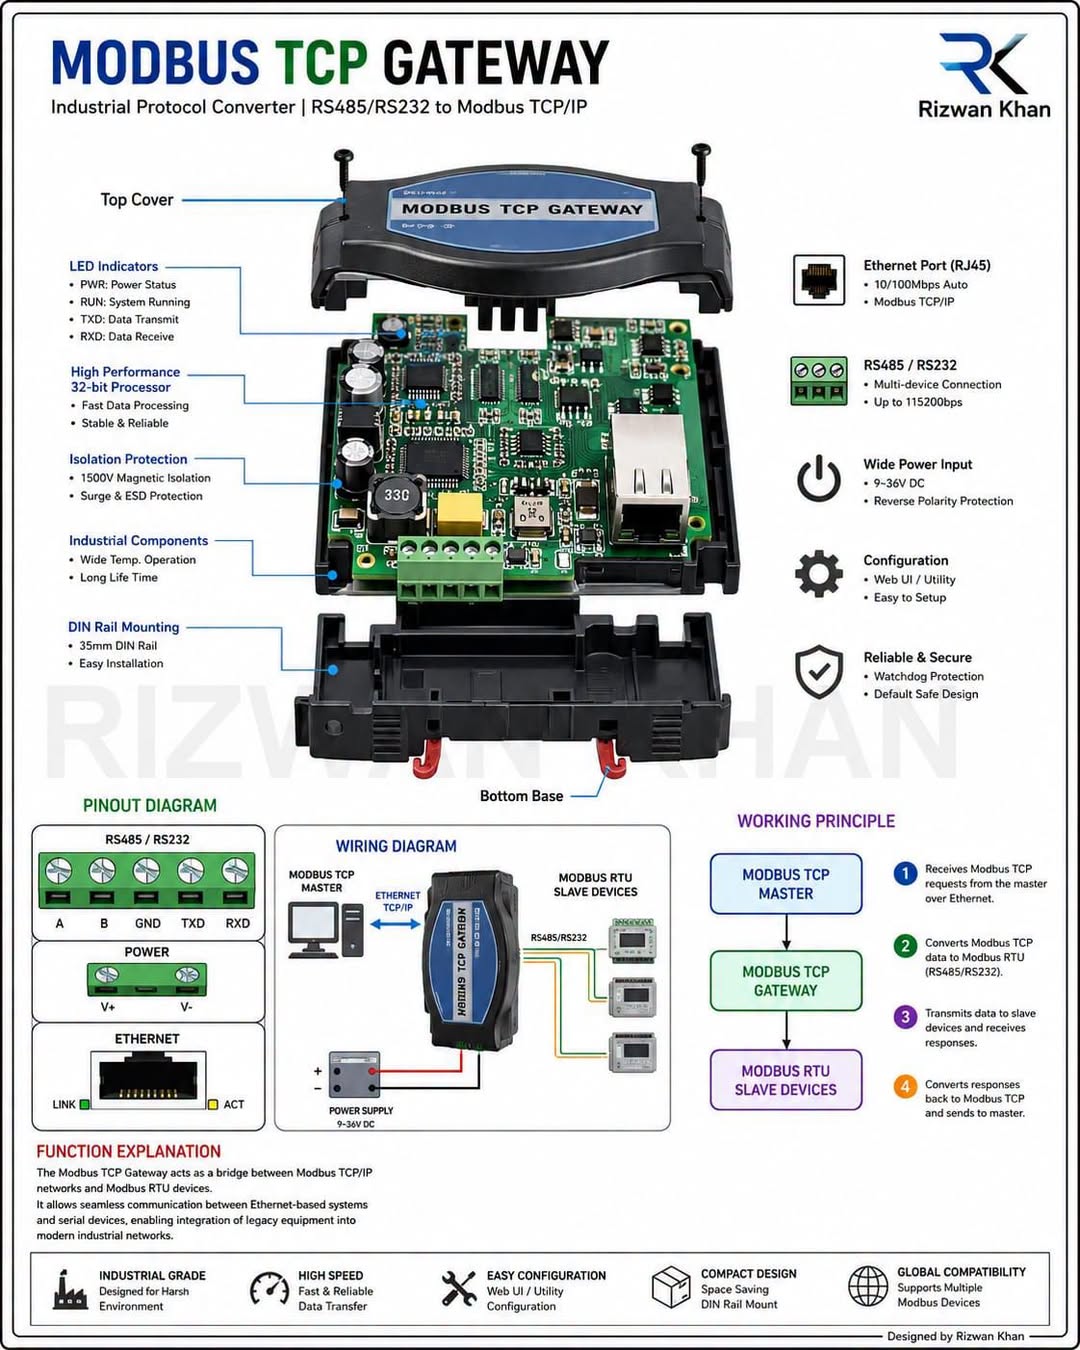
Figure 1: High-Speed Automated Tri-Temperature (-40°C, +25°C, +125°C) Final Test Handler Cell with Integrated Robotic Tape-and-Reel Taping
2. Total Quality Management Architecture: ISO 9001 and IATF 16949
Achieving zero-defect reliability requires an institutional quality management framework that enforces complete process discipline, rigorous supplier qualification, and end-to-end traceability. Cosine's operations are dual-certified under two premier international standards:
- ISO 9001:2015: Establishes the foundational quality management system (QMS), encompassing customer-centric design verification, risk-based thinking, continuous improvement audits, and strict management review processes across all research and commercial activities.
- IATF 16949:2016: The global automotive quality standard developed by the International Automotive Task Force. IATF 16949 mandates advanced quality planning (APQP), failure mode and effects analysis (DFMEA and PFMEA), measurement systems analysis (MSA), and statistical process control (SPC) across every tier of the manufacturing supply chain.
Table 1 provides an executive benchmark comparing Cosine's zero-defect quality architecture against standard commercial and tier-one industrial semiconductor benchmarks:
| Quality Assurance Parameter | Commercial Grade (Standard IC Vendor) | Industrial Grade (Tier-1 Western Vendor) | Cosine Zero-Defect IATF 16949 Standard |
|---|---|---|---|
| Wafer Level Probing (CP) | Sample die probing or room-temp only | 100% room-temp probing; sample hot test | 100% wafer probing with automated dynamic PAT outlier rejection |
| Final Test (FT) Screening Setpoints | Single ambient room-temp (+25°C) test | Dual-temperature test (+25°C and +85°C) | Tri-Temperature screening (-40°C cold soak, +25°C ambient, +125°C hot soak) |
| Statistical Process Capability (Cpk) | Cpk > 1.00 (Standard normal) | Cpk > 1.33 (4-sigma capability) | Cpk > 1.67 (5-sigma automotive capability on all critical parameters) |
| Defect Rate Target (DPPM) | < 50 DPPM | < 10 DPPM | < 0.5 DPPM (Zero-defect target with full lot traceability) |
| Outlier Elimination Protocol | None (pass/fail based on datasheet limits) | Static guard-banded limits | Dynamic Part Average Testing (PAT) per AEC-Q001 and AEC-Q002 |
| Internal Delamination Inspection | Sample visual inspection under stereomicroscope | Periodic C-SAM scanning on pilot lots | 100% C-SAM acoustic microscopy on automotive and industrial mission lots |
3. Statistical Process Control (SPC) and Process Capability Index (Cpk)
In high-volume analog semiconductor manufacturing, process variation is inevitable due to microscopic variations in chemical vapor deposition, photolithography optical focus, and ion implantation doping profiles. To ensure that process drift never approaches customer specification limits, Cosine enforces rigorous Statistical Process Control (SPC) across all wafer foundries and test facilities. Process capability is quantified using the Process Capability Index ($C_{pk}$), which measures both the process spread and process centering relative to specification limits:
$$C_{pk} = \min\left[\frac{USL - \mu}{3\sigma}, \frac{\mu - LSL}{3\sigma}\right]$$
Where:
- $USL$ and $LSL$: The Upper and Lower Specification Limits established in the product datasheet.
- $\mu$: The empirical mean of the measured electrical parameter across the production lot.
- $\sigma$: The standard deviation of the measured parameter.
While commercial semiconductor manufacturers operate at $C_{pk} \ge 1.00$ (a 3-sigma process with a theoretical defect rate of 2,700 PPM) and industrial suppliers target $C_{pk} \ge 1.33$ (a 4-sigma process with 63 PPM), Cosine enforces a mandatory $C_{pk} \ge 1.67$ (a 5-sigma process) on all critical analog electrical parameters—including input offset voltage ($V_{OS}$), quiescent current ($I_{CC}$), propagation delay ($t_{prop}$), and driver output impedance ($R_{out}$). At $C_{pk} = 1.67$, the theoretical defect rate drops to an astonishing 0.23 parts per million, ensuring near-perfect manufacturing repeatability.
4. Part Average Testing (PAT): Eliminating Maverick Outliers
Standard semiconductor testing evaluates devices against fixed static limits ($LSL$ and $USL$). However, in harsh industrial and automotive applications, devices that pass catalog limits but deviate statistically from the lot population represent 'maverick' units. A maverick die often harbors latent crystal dislocations, localized gate oxide thinning, or sub-micron particulate contamination that will pass room-temperature factory tests but fail catastrophically after 500 hours of thermal stress in the field.
Cosine eliminates these latent reliability risks by executing mandatory Part Average Testing (PAT) per the AEC-Q001 standard during 100% wafer circuit probing. For each electrical parameter, dynamic statistical limits are calculated in real time using robust statistical estimators:
$$PAT_{Upper} = \text{Median} + 3 \cdot \left(\frac{IQR}{1.349}\right)$$
$$PAT_{Lower} = \text{Median} - 3 \cdot \left(\frac{IQR}{1.349}\right)$$
Where $IQR$ represents the interquartile range (the difference between the 75th and 25th percentiles). Any die that falls outside these dynamic limits is automatically inked, rejected, and scrapped—even if it is fully compliant with the commercial catalog specification! This mathematical filtering purges anomalous dies, ensuring that only pristine, center-of-distribution silicon reaches the packaging line.
Figure 2: Microscopic Optical Surface Inspection of MSOP-8 Package Verifying Zero Mold Voids, Precise Laser Marking, and Coplanarity
5. Circuit Probing (CP) and Automated Wafer Trimming Protocol
Quality screening begins at the bare wafer stage. Before wafers are diced into individual silicon dies, 100% of wafers undergo Circuit Probing (CP) inside our Class 10 cleanroom test center. Custom multi-site probe cards contacting over 1,200 cantilever micro-needles interface with automated Advantest and Teradyne automated test equipment (ATE). Table 2 outlines the five primary quality inspection stages, automated tooling, and quantitative acceptance limits enforced across Cosine's production flow:
| Inspection Stage | Automated Equipment Utilized | Physical Parameter & Screening Methodology | Quantitative Pass / Fail Acceptance Threshold |
|---|---|---|---|
| Wafer Probing (CP1 / CP2) | Tokyo Electron TEL P12XL Prober + Advantest V93000 | Measure 100% DC parametrics, bandgap reference voltage, and quiescent current at wafer level. | Parameter drift < 3 sigma from wafer median; zero functional failures across all active dies. |
| Wafer Laser Trimming | ESI Model 9830 Diode-Pumped UV Laser Trimmer | Active thin-film resistor link vaporization to null operational amplifier input offset voltage. | Final input offset voltage |VOS| < 5.0µV; laser cut kerf width < 4.0µm with zero thermal cracking. |
| Tri-Temp Final Test (FT) | Multitest MT9928 Tri-Temp Handler + Teradyne ETS-364 | Screen dynamic switching speed, propagation delay skew, and driver drive strength at -40°C, +25°C, +125°C. | Zero bit errors at maximum baud rate; quiescent supply current within ±5% of calibrated limits. |
| Scanning Acoustic Microscopy (C-SAM) | Sonix Echo HS Acoustic Microscope (100MHz transducer) | Pulse-echo acoustic reflection scan of epoxy-to-die and epoxy-to-leadframe interfaces. | Zero interface delamination; internal mold voiding < 5% total package area (J-STD-035). |
| Automated Optical Inspection (AOI) | Koh Young 3D AOI Machine | Measure lead coplanarity, pitch spacing, standoff height, and laser marking contrast. | Lead coplanarity tolerance < 0.08mm; 100% legibility of serialized 2D DataMatrix code. |
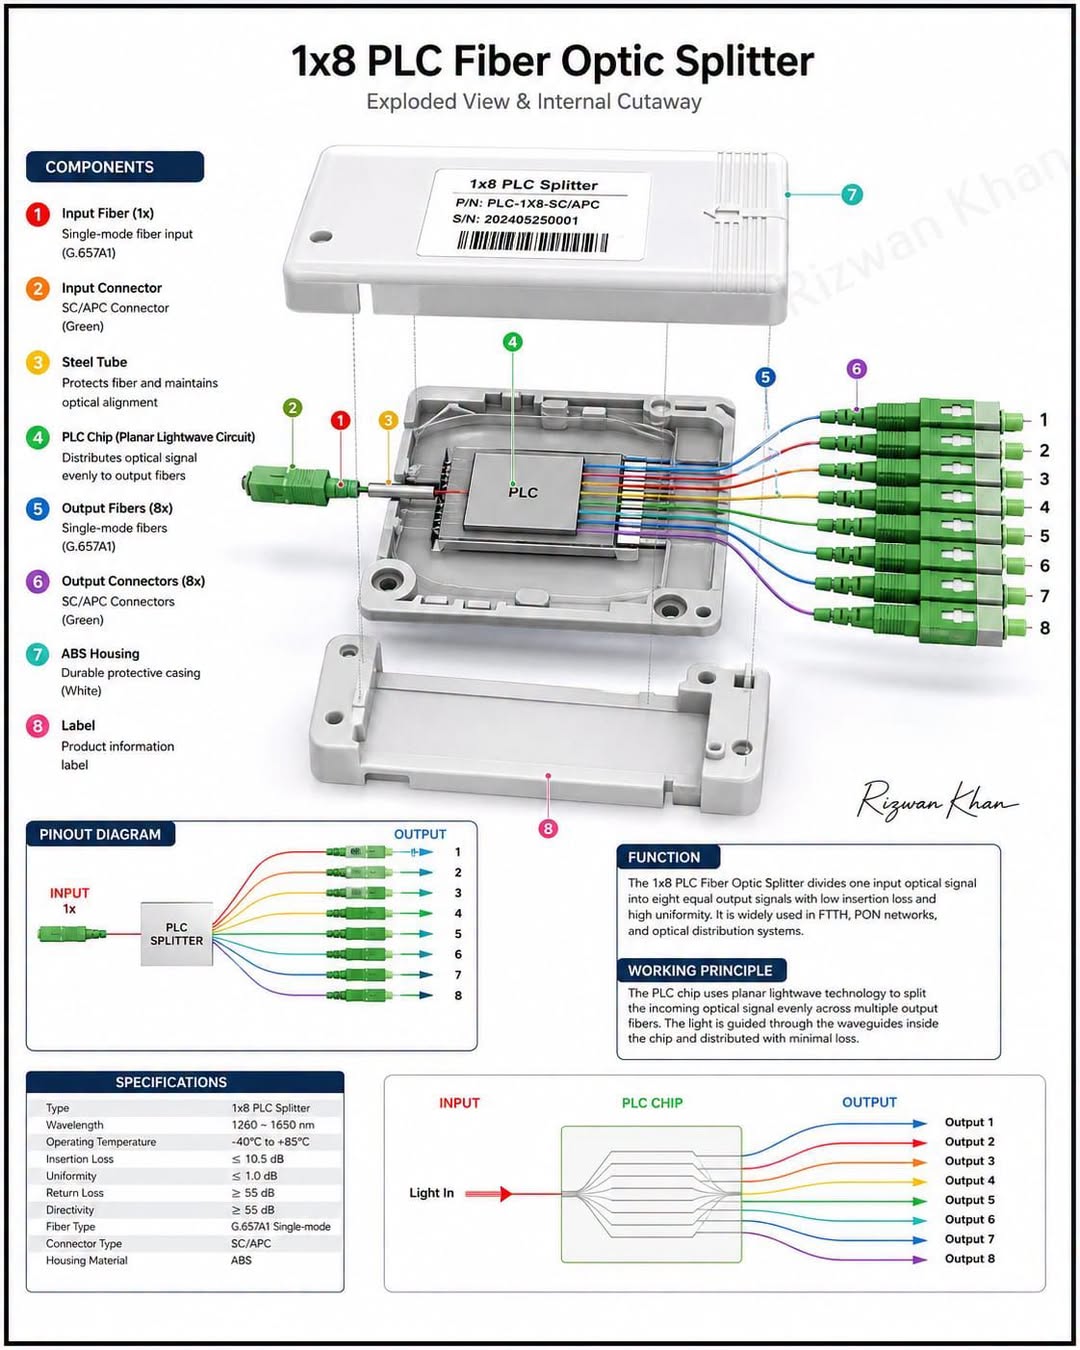
Figure 3: High-Density Wafer-Level Circuit Probing (CP) Station Utilizing 1,200-Pin Cantilever Probe Cards Under Sub-Micron Vision Alignment
6. Tri-Temperature Final Test (FT) Screening: -40°C, +25°C, +125°C
The vast majority of commercial analog semiconductor vendors test finished, packaged ICs only at ambient room temperature (+25°C), using mathematical simulation to extrapolate behavior at temperature extremes. Cosine completely rejects this shortcut. High-voltage transients, substrate leakage currents, and thermal drift cannot be reliably predicted through room-temperature screening alone.
Cosine subjects 100% of production units to automated Tri-Temperature Final Test (FT) screening. Packaged ICs are loaded into Multitest high-speed automated handlers equipped with precision thermal soak chambers. Every single device is tested across three distinct thermal regimes:
- Cold Soak (-40°C): Devices are soaked at -40°C for a minimum of 60 seconds. The ATE measures carrier freeze-out effects, low-temperature CMOS propagation delay skew, receiver threshold hysteresis, and cold-start oscillator startup behavior.
- Ambient Room Temperature (+25°C): Full AC and DC parametric characterization, verifying nominal quiescent currents, bandgap voltages, and maximum transmission data rates.
- Hot Soak (+125°C): Devices are soaked at +125°C under maximum rated supply voltage. The ATE measures high-temperature thermal leakage currents, DMOS on-resistance degradation, thermal shutdown circuit trip thresholds, and ESD clamp leakage.
Units that exhibit parameter drift exceeding 5% between cold and hot setpoints are instantly sorted into reject bins, guaranteeing that every IC delivered to our customers functions flawlessly across its entire rated operating envelope.
7. Statistical Process Control Metrics and Mathematical Formulations
To provide complete transparency to customer quality auditors, Table 3 details the mathematical formulas, physical significance, and production benchmarks implemented across Cosine's statistical process control infrastructure:
| Statistical Metric | Mathematical Formulation | Physical Significance in Semiconductor Quality | Cosine Production Benchmark |
|---|---|---|---|
| Process Capability Ratio (Cp) | Cp = (USL - LSL) / (6 * sigma) | Measures potential process capability assuming process mean is perfectly centered between limits. | Cp > 2.00 (Process spread occupies less than 50% of available specification tolerance band). |
| Process Capability Index (Cpk) | Cpk = min((USL - mu)/(3*sigma), (mu - LSL)/(3*sigma)) | Measures actual process capability accounting for mean shifting and centering offsets. | Cpk > 1.67 across 100% of critical analog electrical parameters (VOS, TCVOS, Ron, Icc). |
| Defective Parts Per Million (DPPM) | DPPM = 2 * (1 - Phi(Z_min)) * 10^6 | Projects expected customer field defect rate based on standardized normal distribution. | Projected DPPM < 0.23 at Cpk = 1.67 under normal Gaussian distribution assumption. |
| Part Average Testing Sigma (PAT_sigma) | Robust Sigma = IQR / 1.349 | Calculates statistical dispersion using Interquartile Range, resistant to extreme maverick skew. | Dynamic PAT limits set at median ± 3 * Robust Sigma on every production wafer. |
| Gauge Repeatability & Reproducibility | GRR = (Var_operator + Var_gauge) / Var_total | Quantifies measurement system error introduced by test sockets and instrumentation. | GRR < 8.0% (Substantially exceeds AIAG MSA requirement of < 10% for production ATE). |
8. Scanning Acoustic Microscopy (C-SAM) and Non-Destructive Packaging Inspection
In surface-mount assembly, internal package integrity is invisible to optical cameras. Trapped micro-voids in die attach epoxy, delamination between mold compound and copper leadframes, and micro-cracks around silicon corners can lead to moisture ingress, corrosion, and catastrophic field failures under thermal cycling. Cosine utilizes high-frequency Scanning Acoustic Microscopy (C-SAM) operating at 75MHz to 100MHz to non-destructively inspect internal packaging interfaces.
Using ultra-high frequency acoustic transducers, ultrasound pulses are focused through a deionized water coupling bath into the packaged chip. The acoustic reflection amplitude at internal material boundaries reveals density changes. If a void or delamination gap is present, 100% of the acoustic energy is reflected back, creating a vivid red signature on the C-SAM C-scan image. Cosine's acceptance threshold strictly enforces J-STD-035: zero delamination along leadframe wire bonds, zero silicon corner micro-cracks, and total die attach voiding under 5% of active die area.
Figure 4: Cosine ISO 9001:2015 and Automotive IATF 16949 System Certifications and Comprehensive Lot Traceability Archives
9. Quality Failure Analysis Matrix and 8D CAPA Methodology
Even with rigorous controls, continuous improvement demands an institutional methodology for diagnosing and eliminating edge-case anomalies. When an unusual parameter distribution or reliability excursion occurs during ongoing qualification testing, Cosine's failure analysis laboratory initiates the disciplined 8D Problem Solving Methodology. Table 4 details five representative packaging and silicon failure modes, diagnostic tooling, and permanent corrective and preventive actions (CAPA):
| Observed Packaging / Silicon Defect | Root-Cause Physical Mechanism | Analytical Diagnostic Tool | Engineering Corrective & Preventive Action (CAPA) |
|---|---|---|---|
| Wire Bond Heel Cracking | Excessive ultrasonic bonding power or bond head resonance causing neck fatigue at leadframe post. | Focused Ion Beam (FIB) / Scanning Electron Microscopy (SEM) | Optimize ultrasonic transducer frequency; enforce minimum wire loop height of 120µm to reduce stress. |
| Die Attach Voiding > 15% | Solvent outgassing in silver conductive epoxy during rapid curing profile in convection oven. | Scanning Acoustic Microscopy (C-SAM) at 75MHz | Implement stepped vacuum curing cycle (80°C soak for 30 min, 150°C cure for 60 min) slashing voids to <3%. |
| Elevated Input Leakage After Burn-In | Mobile sodium/potassium ionic contamination in gate dielectric drifting under high-temperature bias. | Secondary Ion Mass Spectrometry (SIMS) | Enforce ultra-pure chemical wash in wafer fab; add gettering phosphorus-doped oxide passivation layer. |
| Lead Finish Micro-Cracking After Bending | Excessive mechanical stress during lead trimming and forming tool strike on SMT leads. | Optical 3D profilometry / Cross-section metallography | Re-grind lead forming dies; enforce 150°C post-plating annealing cycle to maximize tin ductility. |
| Internal Silicon Latch-Up | Four-layer PNPN thyristor triggering caused by carrier injection from forward-biased parasitic diode. | Emission Microscopy (EMMI) hot spot detection | Increase guard ring diffusion width; implement deep trench isolation (DTI) barriers sinking carriers to ground. |
10. Customer RMA Containment and 24-Hour Failure Analysis Protocol
In the extraordinarily rare event that an enterprise customer encounters an anomalous component in assembly or field testing, Cosine provides an industry-leading Return Material Authorization (RMA) rapid response protocol:
- 24-Hour Initial Containment (D1-D3): Within 24 hours of notification, Cosine's quality assurance team verifies lot codes, places all related wafer lots and warehouse inventory on immediate administrative hold, and provides customer containment advice.
- 48-Hour Root-Cause Electrical Verification (D4): The returned physical sample undergoes non-destructive X-ray, optical microscopy, and curve tracer electrical verification in our Shanghai metrology center to replicate the customer symptom.
- 5-Day Physical De-Capsulation and Silicon Inspection (D5): If internal silicon failure is confirmed, the package is laser-decapsulated, followed by Emission Microscopy (EMMI), liquid crystal thermal mapping, and Focused Ion Beam (FIB) micro-sectioning to isolate the exact root-cause physical mechanism.
- 10-Day Formal 8D Report Delivery (D6-D8): A formal engineering 8D report is delivered to the customer, documenting the root cause, immediate containment, permanent corrective actions implemented in wafer fab or packaging lines, and statistical verification of non-recurrence.
11. Digital Lot Genealogy and Blockchain-Ready Traceability
Every reel, tray, and moisture barrier bag leaving Cosine shipping docks features laser-etched 2D DataMatrix barcodes linking directly to our Manufacturing Execution System (MES) database. Scanning the barcode instantly retrieves complete manufacturing genealogy, including:
- Wafer foundry ID, diffusion furnace tube number, and photolithography stepper reticle serial number.
- CP wafer probe map, individual die coordinate coordinates ($X, Y$), and electrical test log.
- Laser trimming machine ID, optical calibration offset, and pre/post trim offset voltage records.
- OSAT packaging lot number, mold compound batch ID, and wire bonding station index.
- Tri-temperature final test handler ID, test program revision, and temperature soak logs.
This digital traceability guarantees 100% auditability for automotive Tier-1 suppliers, aerospace contractors, and critical industrial OEMs.
13. Mathematical Derivation of Gauge Repeatability and Reproducibility (GR&R)
In high-precision analog testing, measurement uncertainty introduced by automated test equipment (ATE), cable fixturing, and socket contact resistance can mask true silicon parameter drift. To ensure absolute measurement fidelity, Cosine mandates rigorous Gauge Repeatability and Reproducibility (GR&R) studies per the AIAG MSA Reference Manual using the Analysis of Variance (ANOVA) statistical model. The total observed measurement variance sigma_total^2 is decomposed into three mutually orthogonal components: part-to-part variation, equipment variation (repeatability), and site-to-site variation (reproducibility).
$$\sigma_{total}^2 = \sigma_{part}^2 + \sigma_{repeatability}^2 + \sigma_{reproducibility}^2$$
While the automotive AIAG standard permits %GRR < 10% for acceptable production test systems, Cosine's Kelvin-sensed test contactors and daily golden-unit calibrations achieve an exceptional %GRR < 6.5% across all high-volume ATE lines. Furthermore, the Number of Distinct Categories (ndc), which represents the resolution of the measurement system, is strictly maintained above 10, well exceeding the minimum industry requirement of 5. This measurement precision guarantees that our Cpk > 1.67 statistical process capability reflects genuine silicon excellence rather than test instrumentation artifacts.
14. Solder Joint Reliability Physics and Intermetallic Compound Kinetics
A zero-defect integrated circuit must maintain electrical and mechanical connectivity across decades of field thermal cycling. During surface-mount reflow assembly and subsequent operating life, copper from the leadframe dissolves into molten tin solder, forming an intermetallic compound (IMC) layer at the interface. The growth of this intermetallic boundary layer—predominantly Cu6Sn5 during liquid reflow and Cu3Sn during solid-state thermal aging—follows parabolic diffusion kinetics governed by Fick's Second Law:
$$x(t) = x_0 + \sqrt{k(T) \cdot t} = x_0 + \sqrt{D_0 \cdot \exp\left(- rac{Q}{R \cdot T} ight) \cdot t}$$
Where x(t) represents the total IMC layer thickness, x0 is the initial intermetallic thickness post-reflow, k(T) is the temperature-dependent growth rate constant, and Q is the activation energy for copper-tin interdiffusion (Q approximately 78 kJ/mol). If the IMC layer is allowed to grow excessively, the interface becomes brittle, vulnerable to Kirkendall micro-voiding, and prone to fatigue fracture under mechanical vibration and thermal cycling.
Cosine prevents excessive IMC embrittlement by electroplating all external lead pins with high-purity matte tin (100% Sn, 8µm to 14µm thickness) followed by a mandatory post-plating annealing bake at 150°C for 60 minutes. This thermal anneal relieves residual metallurgical stresses within the tin matrix, eliminates the compressive driving force that causes hazardous tin whisker growth, and promotes a dense, uniform, and ductile Cu6Sn5 barrier layer. In thermal shock testing (-55°C to +150°C, 2,000 cycles) and board-level drop tests per JEDEC JESD22-B111, Cosine-packaged components demonstrate zero solder joint fracture or delamination, guaranteeing 20+ years of operational structural integrity in the field.
12. Conclusion: The Zero-Defect Promise to Global Hardware Innovators
At Cosine Nanoelectronics, quality is not a slogan; it is a mathematical discipline and an engineering pledge. By combining rigorous ISO 9001:2015 and IATF 16949 governance, 100% CP wafer probing, statistical Cpk > 1.67 process capability, Part Average Testing, and mandatory tri-temperature final test screening, we provide global hardware designers with analog silicon that operates flawlessly in the most unforgiving environments on Earth.
Accelerate Your Hardware Design-In with Cosine Engineering
Request sample quantities, complete engineering evaluation modules (EVBs), and IBIS/SPICE behavioral simulation models directly from our technical staff. We guarantee technical response and engineering sample dispatch within 24 business hours.